

A tabletop automatic bagger makes sense when your parts are light, your batches are small, and changeover eats more time than the seal cycle. It stops making sense when parts are heavy, bags are wide, or you need more than roughly 15 bags per minute on a steady basis. The tabletop P350S runs 8–15 bags per minute; actual output depends on part shape, loading rhythm, and whether an operator or a feeder loads the bag. If your line is limited by changeover and loading, not peak cycle rate, a tabletop unit is the right size to evaluate. If peak rate is your binding constraint, look at a floor-standing frame instead.
Why the bag opening and seal set the real limit
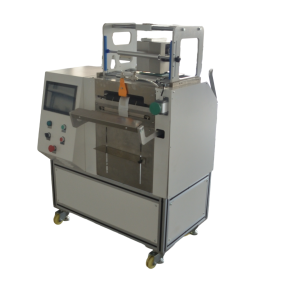
The tabletop automatic bagger pulls a single-side pre-opened roll bag, opens one side, drops the part in, seals with servo torque, and prints inline. Each step has a physical limit. A bag that opens only 60 mm wide will not accept a 70 mm connector body regardless of cycle rate. A seal that runs too hot on 40 µm PE film will burn through before the cooling step finishes. Servo torque sealing with 360-degree wrap heating and air cooling targets consistency: thin film must not burn through, thick film must not under-seal. Verify with a trial seal on your own film, not from a spec sheet.
The inline print step matters on high-mix work. Because the print head is built into the bagger, you produce variable data on demand, one code per bag, instead of stocking pre-printed bags or running a separate label step. That removes one handling pass per bag. It also means the TTO head and the film surface must be matched, and a mismatched ribbon is a common cause of patchy or non-scannable codes. Check the ribbon width against the printhead before you commit to a bag size.
Four industry scenarios and the check that decides each one
Sensors and electronic components. Parts are light, usually under 100 g, and often static-sensitive. The bag must open cleanly without dragging the part. Run a 30-bag trial with your actual component and watch for parts that catch on the bag lip. If the pick-and-open step stalls more than once in 30 cycles, adjust bag width or film stiffness first. A wider bag is not always the fix; a stiffer film may open more reliably on small flat parts.
Automotive parts and hardware. Fasteners and small brackets often need one code per bag for traceability. This is where inline printing earns its place. The TTO print areas of 53×55 mm, 55×115 mm, and 107×115 mm cover different label content; the 107×115 mm head covers larger label content in one pass. Confirm the code size against your scanner at the actual print resolution before ordering. A code that scans on a flat sheet may not scan on a curved PE bag.
Medical kits and appliance accessories. These are multi-part kits with frequent SKU changes. Changeover time, not speed, governs the line. The recipe library stores product recipes recalled from the touchscreen; the official figure is hundreds of recipes, so bag size and print content change without re-programming. Time a real changeover from SKU A to SKU B, including bag roll swap and print content recall. If it exceeds the time you spend bagging one batch, the changeover design needs review.
Small-batch export packing. Bag cost and consumable fit often decide the model. Single-side open roll film is pre-opened on one side and perforated on the other; width, length, thickness, and print are customized to the pick mechanism and sealing parameters. Ask for a film sample matched to your part, not a catalog grade. A film that runs well on a competitor’s machine may not match the JYZN pick mechanism.
Tabletop automatic bagger comparison by scenario
| Scenario | Typical part weight | Binding constraint | Model to evaluate | Verification action |
|---|---|---|---|---|
| Sensors, electronic components | Under 100 g | Bag opening reliability | JYZN-P350S | 30-bag trial, count opening stalls |
| Automotive parts, hardware | 100–500 g | Code scannability | P350 with TTO head matching code size | Scan 20 codes at line speed |
| Medical kits, appliance accessories | 50–300 g per kit | Changeover time | JYZN-P350S with recipe library | Time A-to-B changeover, including film swap |
| Small-batch export packing | Varies | Bag and film cost | P350 or P350S, film sample matched to part | Trial seal on your own film, check seal strength |
The tabletop frame uses casters, so one operator can move it between stations. That matters when you run the same SKU on two lines in a week. It also means the machine can be interfaced with robot arms, weigh feeders, vibratory feeders, and MES/ERP systems when volume grows. Check the interface list against your plant network before you assume the tabletop unit is a dead end.
Acceptance actions before you sign
Run these checks on your own parts and film, not on demo material. A machine that passes on demo film can fail on your 40 µm PE.
- Seal trial: run 20 seals at the low and high end of your film thickness range. Pull each seal by hand and check for channels or burn-through. Thin film must not burn through; thick film must not under-seal.
- Opening trial: run 30 bags with your part. Record any stall, double-feed, or part hang-up. A stall rate above 1 in 30 needs a bag or film change.
- Print trial: print 20 codes at line speed and scan each with your production scanner. A patchy code is usually a ribbon-to-film mismatch, not a head fault.
- Changeover timing: move from your smallest bag to your largest bag, including print content recall. Time it with a stopwatch. Compare against one batch run time.
- Safety check: confirm the dual-zone design. The low-pressure zone should prevent unexpected start-up; the torque-limited high-pressure zone should trip if the seal meets abnormal resistance. Test the high-pressure trip with a small obstruction, following the manual.
Record each result in a table with pass/fail and the film batch number. That record becomes your baseline for the first service call.
Cost and changeover impact
On small batches, changeover downtime usually costs more than peak speed. A line that runs 10 bags per minute but takes 20 minutes to change over loses more than a line that runs 8 bags per minute and changes over in 5 minutes. Run the arithmetic with your own batch sizes. If your average batch is 200 bags, a 20-minute changeover adds 6 seconds per bag. That is comparable to the difference between 8 and 15 bags per minute.
Consumable fit is the second cost lever. Single-side open roll film is customized to the pick mechanism and sealing parameters, so a film that is 5 µm too thick can change seal behavior and scrap rate. Thermal transfer ribbon must match the printhead width and the film surface. Keep one ribbon SKU per printhead width in stock rather than substituting a wider ribbon. A wider ribbon can wrinkle and produce non-scannable codes.
Evaluate changeover time, bag cost, and consumable fit together. Peak speed is the last number to look at, not the first.
Common questions from the floor
Can a tabletop automatic bagger handle 500 g parts?
Sometimes, but check the bag opening and seal cycle at that weight. A heavier part drops faster and can pull the bag lip. Run a 30-bag trial with the actual part before you commit. If the part hangs more than once in 30 cycles, move to a floor-standing model with a wider opening.
Do I need a separate label printer if I add the TTO head?
No. Printing is built into the bagger, so variable data is produced on demand, one code per bag. That replaces the separate label step. Keep a backup ribbon SKU and a spare printhead on the shelf, because a worn head stops the line.
How many recipes does the library hold?
The official figure is hundreds of recipes. What matters is recall time, not the count. Time a recall on the touchscreen with your own bag size and print content. If recall takes longer than a bag roll swap, the recipe library is not saving you time.
What film thickness should I trial first?
Start with the thickness you already buy for hand bagging. Run a seal trial at the low and high end of that range. If the thin end burns through, reduce temperature before changing film. Film changes are slower and more expensive than a setpoint change.
Send your bag drawing and a photo of the part. We will come back with a model recommendation and a reference price band within one business day. Contact us for a quote.
获取报价和机型推荐
请提供以下四项内容,这样我们就能一次性提供产品模型和参考价格区间,而无需花一周时间反复沟通:
- 背包尺寸(宽×长)或你今天使用的背包照片
- 零件尺寸、零件重量以及每袋装多少个
- 每分钟的袋装产量目标,以及每天的运行小时数
- 每袋是否都需要印上日期代码、批号或二维码
我们将在2个工作小时内回复,并在一个工作日内提供型号推荐及参考价格区间。如果您想先查看压印效果,请寄送一个样品零件,我们将为您制作一个试制袋。.