

The rule that saves the most rework: run acceptance on the exact film and part you will produce, not on demo material. Pre-opened bags on a roll bagging machine fail acceptance for three repeatable reasons, and all three are measurable before you sign.
Below are the three wrong calls buyers make when specifying pre-opened bags on a roll bagging machine, why each one is wrong, and the checks that replace them.
Wrong call 1: judging the line by its peak bag count
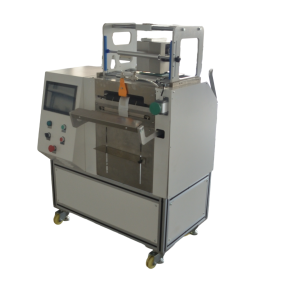
The tabletop JYZN-P350S runs 8–15 bags per minute. That figure moves with part shape, loading rhythm, and whether an operator or a feeder loads the bag. Treat it as a range to qualify, not a number to buy.
High-mix lines are limited by changeover and loading, not by peak cycle rate. A machine that hits 15 bags per minute for one SKU but needs 40 minutes of setup between SKUs loses more hours than it wins.
Test it this way. Time three changeovers between real SKUs: bag size, seal temperature, and print content. Verify the recipe library recalls the correct bag length and code layout from the HMI without re-entering parameters. Then run a 60-minute production block at your normal loading pace and count finished, sealed, coded bags, not strokes.
| Item | Worthless number | Worth measuring |
|---|---|---|
| Speed | Peak cycles/min | Accepted bags/hour at real loading pace |
| Changeover | Best-case demo swap | Minutes from last good bag of SKU A to first good bag of SKU B |
| Code | Print sample on smooth paper | Scan rate across 30 consecutive bags on your film |
Wrong call 2: blaming the film when the pick or seal fails
Single-side open roll film is pre-opened on one side and perforated on the other. Width, length, thickness, and print are customized to the pick mechanism and the sealing parameters. If a bag opens poorly or seals unevenly, the cause is often a mismatch between film and machine settings, not a bad roll.
Servo torque sealing with 360-degree wrap heating and air cooling exists for one reason: thin film must not burn through, thick film must not be under-sealed. Ask what film your supplier runs and demand a trial seal on yours. A spec sheet says nothing about your PE or PET stack.
Run a three-step film trial. Open 50 bags with the production pick vacuum and record misfeeds. Seal at the middle of your temperature window and peel-test 10 bags by hand, looking for tunneling or stringers. Inspect the perforation line after sealing to confirm the bag tears cleanly and the seal does not sit on the perforation.
The single-side open roll film and the bagger should be selected as one system. Changing film suppliers later without retesting the seal is where sealing faults come from.
Wrong call 3: accepting a good bag from one sample shift
One clean sample proves the machine can do it once. Acceptance needs proof it repeats across bags, operators, and hours. Run a continuous block of at least 300 bags at your normal pace and keep every rejected bag. Sort the rejects by cause: open failure, seal fault, print defect, transport jam.
Print is part of the same test. A thermal transfer ribbon must match the printhead width and the film surface, and a mismatched ribbon is the most common cause of patchy or non-scannable codes. Scan 30 consecutive codes with your own scanner and record failures. For larger label content in one pass, confirm the head you ordered: 53×55 mm, 55×115 mm, and 107×115 mm heads are available across the range, not all fitted as standard.
One more check that buyers skip: the dual-zone safety design. The low-pressure zone prevents unexpected start-up and the torque-limited high-pressure zone gives overload protection if the seal meets abnormal resistance. Trip both during acceptance, not on day one of production.
Sign-off checklist
- 30 bags opened with production vacuum; misfeed count recorded
- 10 peel tests across the temperature window, root cause written for each failure
- 300-bag continuous run, reject list sorted by cause
- Three changeovers timed, recipe recall verified on screen
- 30 codes scanned, poor reads kept as samples
- Both safety zones tripped and reset
- Sealed bag measured: seal width and seal position against bag edge
- Film and ribbon lot numbers logged against test results
Evaluate changeover time, bag cost, and consumable fit together before you finalize the model. The JYZN-P350S suits light, high-variety parts such as sensors, fasteners, and medical kits where the operator loads by hand. For the wider family, compare the pre-opened roll bag packaging machine range against your bag drawing before shortlisting.
FAQ
How many bags should we run before accepting the machine?
At least 300 continuous bags at normal pace, plus a separate 30-bag open test and 30 scans. Fewer bags hide intermittent faults in the pick and seal sequence. Sort every reject by cause so the supplier fixes the mechanism, not just the symptom.
Can we keep using our current film on a new bagger?
Possibly, but confirm it. Send the film width, thickness and open-side construction to the machine supplier, then run a trial seal and pick test before committing. Single-side open roll film is customized to the pick mechanism and sealing parameters, so a film that worked elsewhere may not open cleanly here.
Why do our codes look patchy on the sealed area?
Usually a thermal transfer ribbon that does not match the printhead width or the film surface. Check the ribbon-to-head matchup first, then print timing relative to sealing. Scan 30 consecutive codes and keep the poor reads as samples for the supplier.
Do we need the largest print head?
Only if you need larger label content in one pass. The 107×115 mm head covers larger content single-pass, while smaller heads fit short codes and tighter spaces. Print areas of 53×55 mm, 55×115 mm and 107×115 mm are options across the range, not standard on every model.
Is a feeder required to reach the rated speed?
Not required, but it changes output. The P350S runs 8-15 bags per minute, and the actual rate depends on part shape, loading rhythm and whether an operator or a feeder loads the bag. Measure with your real loading method.
Send your bag drawing and a photo of the part. We will come back with a model recommendation and a reference price band within one business day. Contact us for a quote.
获取报价和机型推荐
请提供以下四项内容,这样我们就能一次性提供产品模型和参考价格区间,而无需花一周时间反复沟通:
- 背包尺寸(宽×长)或你今天使用的背包照片
- 零件尺寸、零件重量以及每袋装多少个
- 每分钟的袋装产量目标,以及每天的运行小时数
- 每袋是否都需要印上日期代码、批号或二维码
我们将在2个工作小时内回复,并在一个工作日内提供型号推荐及参考价格区间。如果您想先查看压印效果,请寄送一个样品零件,我们将为您制作一个试制袋。.